Project Details
Pipe Inputs
T1 is not auto-calculated. This version calculates the required bead-up size from ISO and lets the welder record the observed bead-up time after the bead is achieved.
Machine Inputs
Area is total effective ram area. Drag pressure will be converted internally if entered in bar.
Butt Fusion Parameters
Interface Area Ai
—
—
Bead-up / Fusion Pressure
—
—
Heat Soak Pressure P2
—
—
Cooling Reduced Pressure
—
—
Minimum Bead-up Size
—
—
Heat Soak Time
—
—
Plate Out / Change-over
—
—
In-machine Cooling
—
—
Calculate parameters first.
Welding Time & Pressure Diagram
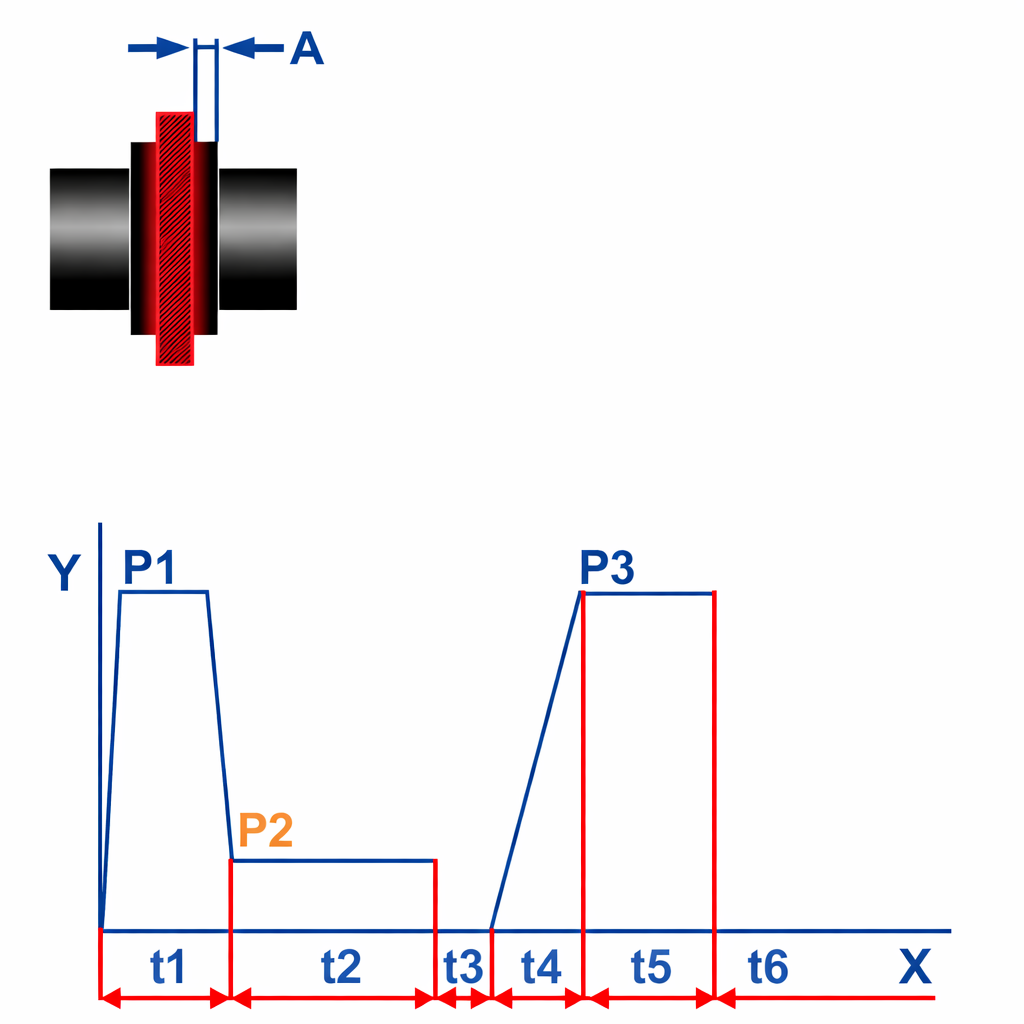
Visual guide of the time stages and pressure steps. The active timer sequence changes with the selected ISO procedure.
Calculation Breakdown
Select pipe inputs and click Calculate Parameters.
Disclaimer
This calculator applies ISO 21307:2017 process logic for SLP, DLP and SHP. SDR and DN availability have been expanded to align with the AS/NZS 4130:2018 Series 1 SDR range from SDR 41 to SDR 7.4. The user must still verify pipe dimensions, machine condition, ambient effects, pressure readings, operator competency, manufacturer requirements, and any project-specific welding procedure before welding.
Countdown Timer
Stage
—
Remaining
—
Next
—
Controls
Calculate parameters first.